Manual visual inspection frequently shows up, disguised, in key expense lines on the P&L. It shows up in direct labor, QA overhead, scrap, re-inspection, and deviation investigations. As critical, it also shows up as regulatory risk that only becomes visible when something goes wrong. That’s a big part of why it survives, spread over expense categories that appear manageable on their own. But add them up on a single sterile injectable line, and they can reach several million dollars a year.
This guide details where visual inspection costs come from, including the one most models leave out entirely: inspecting at human speed. We then cover how to quantify the total inspection expense for your own operation and where manual inspection still earns its place. The figures are illustrative, drawn from The CFO’s Guide to Inspection ROI and from public benchmarks. This is simply a starting point for your own numbers, not a replacement for them.
In this guide, you will learn
- Why manual inspection is still the default in pharmaceutical inspection
- What a compliant manual inspection program actually requires
- The seven sources of cost in a typical manual inspection
- The capacity limitations and cost of inspecting at human pace
- How limitations in visual inspection can create sources of regulatory exposure
- How to understand the total cost of visual inspection: a single-line estimate
- How to estimate the impact AVIS can bring to your production line
- Where manual inspection still makes sense
- How to quantify the benefits of automated inspection
- Frequently asked questions
Why manual inspection is still the default
The FDA’s December 2021 draft guidance on visible particulates specifies that each final container must be inspected using a qualified, documented method. The EU GMP Annex 1 sets the same expectation. For decades, trained human inspectors were the only method that could meet this guidance, and they have been the most effective way to meet that requirement, as a qualified inspector can inspect a new container, a new formulation, or a cloudy suspension without an engineering project.
Manual inspection is also the benchmark against which visual inspection alternatives are measured and evaluated. Annex 1 requires that automated systems be validated as performing at quality levels equal to or better than manual inspection systems. That’s a reasonable standard, and it’s one reason manual inspection persists even at sites that have invested in automated systems.
The real question isn’t whether manual inspection works. It’s where it performs best in quality and cost, and what it costs to keep it performing at the level regulators now expect.
What a compliant manual program actually requires
The USP <1790> regulation and the informational chapter alongside USP <790> outline what a compliant manual inspection should look like. The details matter here because each one adds up, and can add up significantly.
- Lighting. At least 2,000 to 3,750 lux at the point of inspection for clear glass containers.
- Pace. A reference time of 10 seconds per container, 5 seconds each against black and white backgrounds.
- Breaks. A break from inspection at least every hour, based on industry experience with fatigue.
- Vision. Inspectors with 20/20 vision (corrected if needed) who pass a color deficiency test, re-evaluated every year.
- Qualification. Testing against defect standards, where an individual inspector may not miss a critical defect.
Annex 1 adds its own layer of complexity: it requires controlled illumination and background, specified inspector workloads, and annual line qualification using the manufacturer’s defect library, including inspector eyesight checks. None of this is unreasonable. All of it takes people, time, and documentation.
The seven cost layers of manual inspection
Direct labor and headcount
The fully loaded cost of using qualified visual inspectors typically runs between $80,000 and $130,000 a year. A production line manually inspected around the clock, five days a week, will need 12 to 20 inspectors. That puts direct labor for a single manually inspected line at roughly $1.5 million to $2.5 million a year.
Throughput objectives explain the headcount requirements and related expense. At the USP reference time of 10 seconds per container, one inspector can handle 360 containers an hour before breaks, handling, and paperwork, and published re-inspection rates of 3,000 to 6,000 units per inspector-day reflect that pace. As a result, when volume goes up, headcount goes up.
The loaded rate is an important labor expense consideration. Every inspection team shoulders a second set of labor costs: the supervisors, trainers, and the QA staff who run qualification and requalification. And then there’s the documentation that proves each inspector is fully trained. On top of that are shift premiums and overtime to cover vacancies. These expenses are rarely lumped into the same budget line as the inspectors themselves, which is one reason manual inspection often looks cheaper on paper than it is.
Turnover, qualification, and inspector ergonomics
Training a new inspector can take 6 to 12 months to become fully qualified. Yet annual turnover in production environments is often 20 to 40%. So for a team of 15 inspectors, that can mean replacing and training three to six people a year. Each replacement restarts the qualification cycle and creates a temporary capacity gap. The training program, the defect kits it depends on, and the annual requalification of everyone else are costs that never really go away.
One critical factor in manual inspection is how turnover and ergonomics connect, and how they limit production efficiency. Manual inspection requires an inspector to maintain close visual attention on a stream of unit after unit for most of a shift. FDA’s 2021 draft guidance says the environment for manual and semi-automated inspection should be ergonomically designed for inspector comfort. Further, USP <1790> recommends a break at least every hour because performance naturally drops as fatigue builds.
But human inspection is inherently flawed, as even a momentary glance away from the booth can let a defective unit pass unseen. This risk is compounded by pressure to raise throughput, which cuts the time spent on each unit. A site can manage all of this well. It can’t make the job less demanding, and demanding, repetitive roles are hard to keep staffed.
The cost shows up in three places: the lost capacity due to required breaks and inspector rotation, the line qualification cycle that restarts every time an inspector leaves, and the accuracy that naturally drops late in a shift, which is the reason many sites add a second inspection pass in the first place.
False rejects and lost yield
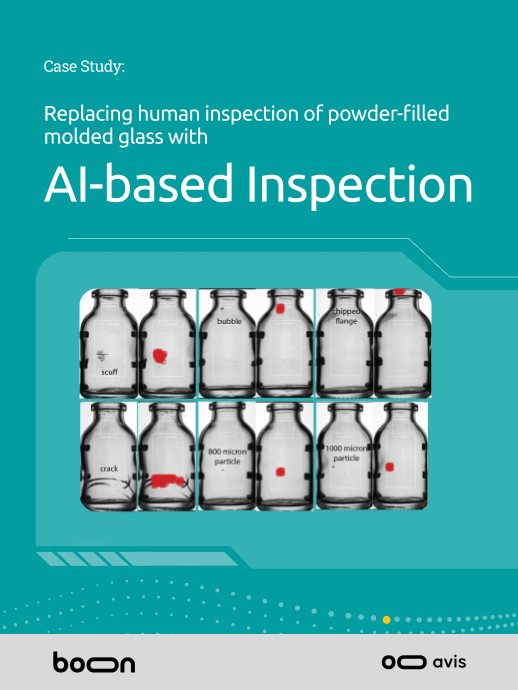
False rejects are usually the biggest source of lost yield and are costly. On complex products, lyophilized cakes, powder fills, suspensions, and molded glass, manual inspection produces false reject rates in the 10 to 20% range, because inspectors sensibly reject anything that looks uncertain. Every one of those units is compliant product written off.
For example, with a line producing 5 million units a year at $10 of finished-goods value per unit, changing from a 10% to a 3% false reject rate can recover roughly $3.5 million a year. At $50 a unit, a realistic figure for many sterile injectables, the same improvement becomes $17.5 million.
Re-inspection and the second pass
Because manual inspection has inherent accuracy variations due to inspector fatigue and differences from one inspector to the next, many sites add the expense of a second 100% inspection pass. This tightens AQL sampling to offset the limitation, but rejected units compound the challenge, often going back through manual re-inspection as well. Every extra pass takes time and capacity, consumes direct labor, and draws on the same trained inspectors. It’s no surprise that production costs scale with reject volume, so it’s worth modeling from your own reject and re-inspection rates rather than a benchmark.
Deviations and investigations
Each batch that triggers a reject alert reduces production capacity through investigation time. This includes time for QA review, to generate documentation updates, and often a batch hold while all this is taking place. It’s that simple, but difficult to track and quantify.
It should be no surprise that a typical pharmaceutical alert can cost anywhere from $5,000 to $50,000 fully burdened to resolve, and a full investigation with batch analysis and disposition can exceed $100,000. This can add up quickly: a production line having one inspection-driven deviation a week, averaging $30,000 in additional costs, can consume up to nearly $1.5 million a year in QA and validation capacity.
Working capital tied up in held product
Product waiting on re-inspection is finished goods that can’t be released. On a $50-a-unit line producing 5 million units a year, cutting the average re-inspection turnaround by 30 days frees up roughly $20 million in inventory. It’s a balance-sheet cost rather than a P&L one, which is exactly why it tends to be left out.
What gets through
The least visible but most costly expense in manual visual inspection is the missed defect that passes inspection. For a 100-micron particle, the probability of detection in a seeded standard is around 40%. High-performing visual inspection detection, typically defined as 70% or better, frequently begins at 150 microns. You can see this as the best-case outcome from trained inspectors working under ideal conditions.
A defective unit that escapes visual inspection creates real costs that are hard to quantify until the defect flows into finished goods as a passed product. It shows up as a field complaint, a recall notice and campaign, or even an FDA observation. A Knapp study benchmarked manual inspection against AVIS, and AVIS delivered 88% fewer falsely accepted defects.
The capacity cost of inspecting at human pace
Manual inspection costs limit production capacity and qualified production throughput. According to one industry executive quoted in Pharma Manufacturing in August 2026, a manual inspector can examine at most four syringes per minute, compared with a qualified AI system that can check 400. The throughput will vary across production lines and products, but it is a compelling difference.
A relevant current example is GLP-1 and incretin therapies, which have become major contributors to growth in the pharmaceutical industry. For these two blockbuster products, the drive to expand production has reshaped the contract manufacturing market. Even so, demand continues to outrun supply, so significantly that the FDA permitted 503B outsourcing facilities to compound them until the shortages were resolved.
For most CDMOs and sterile manufacturers, the pressure isn’t only on the high-volume product line itself, which is typically built for high-speed production with automated equipment. The pressure is broader: competing capacity for the same fill-finish time, for the same QA team, and for the same pool of qualified inspectors. The key limiting factor becomes a line that can’t release product faster than its inspectors can clear it. The cost isn’t a line item, it’s the opportunity cost of a contract the site can’t take on. And that capacity goes to a competitor.
A straightforward way to estimate how many additional batches a year the line could release if inspection weren’t the constraint is to multiply the number of batches by their margin. The CFO’s Guide uses a related measure. On a fill line valued at $4,000 an hour and running 6,000 hours a year, a 5-percentage-point improvement in overall equipment effectiveness is worth roughly $1.2 million in additional capacity.
Regulatory exposure
Understandably, annual inspection errors tend to increase as SKU counts grow and staff turnover rises. A case in point comes from France’s ANSM, which reported 319 Annex 1 non-conformities across 30 sterile manufacturing sites inspected between 2023 and May 2025. Key factors included missing trend thresholds by defect type, AQL criteria that didn’t treat critical defects as rejects, and re-inspection carried out without identifying root causes.
Each finding requires an expensive remediation program. If a Form 483 is issued, the manufacturer must respond within 15 business days, drawing attention and resources off the production line. The cost of a remediation program commonly runs from $1 million to more than $10 million, including consulting, re-validation, and leadership time.
Putting it together: a single-line estimate
The table below pulls the layers into one view for a representative line of 5 million units a year at $10 per unit, unless noted.
| Cost layer | What drives it | Illustrative figure |
|---|---|---|
| Direct labor | 12 to 20 inspectors per line at $80K to $130K fully loaded | $1.5M to $2.5M a year |
| Turnover, qualification, and ergonomics | 6 to 12 months to qualify; 20 to 40% annual turnover; hourly breaks | 3 to 6 replacements a year on a team of 15, plus break and rotation capacity |
| False rejects | 10 to 20% false reject rate on complex products | About $3.5M a year recovered moving from 10% to 3% ($17.5M at $50/unit) |
| Re-inspection and second pass | 100% plus 100% passes; 3,000 to 6,000 units per inspector-day | Scales with reject volume; model from your own rates |
| Deviations | $5K to $50K each; $100K+ with full investigation | About $1.5M a year at one per week |
| Working capital | Held product awaiting re-inspection | About $20M released per 30 days faster ($50/unit line) |
| Capacity | Inspection pace limits how fast the line can release product | About $1.2M per 5 points of OEE on a $4,000/hour line |
| Escapes and regulatory | Probabilistic detection; 483 remediation of $1M to $10M+ | Event-driven; sits outside the annual run rate |
These layers overlap in places, so don’t simply add the rows. The CFO’s Guide to Inspection ROI builds them into a single five-year model.
How to estimate your own number
The good news is that most production sites already have more than enough accessible data to build a first-pass estimate. And it’s not time-consuming; it often takes an afternoon, not a consulting engagement.
- Count the people. Quantify inspectors per shift, number of shifts, and the fully loaded cost. Then add supervisors, trainers, and the QA time spent qualifying inspectors.
- Quantify the cost of rejects. Multiply total annual units by your current false-reject rate, then by the finished-goods value per unit. If you don’t track false rejects separately from true rejects, re-inspecting a sample of rejected units will give a good working estimate.
- Add re-inspection. Quantify the units sent back through manual inspection, divide by units per inspector-day, then multiply by the inspector’s daily loaded cost.
- Count the deviations. Quantify the inspection-driven deviations over the last 12 months, then multiply by your average fully loaded cost per deviation.
- Note the working capital. Quantify the number of days, and the cost, that product waits on re-inspection instead of being shipped.
- Price the capacity. Estimate the additional batches the line could release each year if inspection weren’t the bottleneck, and multiply by the margin on those batches.
- Keep the risk line separate. Quantify inspection escapes, product recalls, and remediation actions. These don’t belong in the production run rate because they overstate the volume, but they are critical to discuss in the conversation with finance.
It’s why we designed the AVIS ROI Calculator to take these same inputs and produce a line-specific view, with capex and opex subscription options modeled side by side.
Where manual inspection still makes sense
None of this means manual inspection should disappear; it can still be the right tool in several places.
- As the benchmark. Annex 1 requires automated systems to prove themselves against manual performance, so a qualified manual capability is part of validating any automated one.
- For AQL sampling and investigations. Human review of AQL samples and rejected units during an investigation stays valuable even on fully automated lines.
- For very small or one-off batches, where setup of any kind costs more than the inspection itself, and for products not yet qualified on an automated system while that qualification is under way.
For most sites, the goal isn’t zero inspectors. It’s moving people off repetitive 100% inspection, where fatigue and variability can’t be engineered away, and onto oversight, investigation, and AQL work, where their judgment adds the most.
What changes with automated inspection
Automation can shift some or most of the cost that scales with volume and headcount into a fixed, predictable cost. However, legacy rule-based AVI still produces false reject rates of 10 to 30% on complex products. Additionally, both rule-based and supervised AI systems take weeks to months to build each recipe before production can even begin. This is why these legacy systems need volumes of around 10 million units a year per SKU to operate profitably, and why so many products stay on manual inspection.
AVIS is designed to deliver that performance without the legacy trade-offs. AVIS typically trains on just 500 compliant units and builds a recipe in under 60 minutes. Once in production, it performs with documented false reject rates of 1 to 6% on complex formats. The model can be locked after qualification, and every inspection event and recipe change is captured in a 21 CFR Part 11 audit trail.
Bringing an AVIS line into production typically takes about six weeks from purchase order. On a 5-million-unit, $10 base case, the CFO’s Guide models a five-year NPV of about $24.9 million at a 10% discount rate, with payback inside five months on a $2.5 million investment.
Frequently asked questions
How many inspectors does a manual inspection line need?
It depends on the line’s production volume, the shift size and complexity, and especially the container type being inspected. For a line inspected 24 hours a day, five days a week, it can need 12 to 20 qualified inspectors.
What is a typical false reject rate for manual inspection?
For complex products such as lyophilized, powder-filled, and suspension formats, published false reject rates run from 10 to 20%.
Is manual visual inspection still compliant?
Yes. FDA, USP, and EU GMP all allow manual inspection by trained, qualified inspectors under controlled conditions. The requirements around lighting, pacing, breaks, qualification, and trending are what make it expensive to do well.
Does moving to automated inspection mean building a defect library?
Not with AVIS. The model trains only on compliant product. Qualification still requires challenge testing with representative defects, as Annex 1 expects of any automated system, but there’s no labeled training library to build or maintain.
Why does GLP-1 demand matter to sites that don’t make GLP-1s?
Because it competes for the same fill-finish capacity, QA resources, and qualified inspectors. When capacity is tight, any step that runs at human pace becomes more expensive, whatever product is on the line.
Where should we start to size the opportunity?
Start with false rejects. It’s usually the largest layer, and the easiest to estimate from data you already have.
Sources
- U.S. Food and Drug Administration. Inspection of Injectable Products for Visible Particulates, draft guidance for industry (December 2021).
- United States Pharmacopeia. <1790> Visual Inspection of Injections (briefing text).
- European Commission. EU GMP Annex 1, Manufacture of Sterile Medicinal Products (2022), sections 8.30 to 8.33.
- PDA Letter. Reducing Human Error for Manual Visual Inspection, V. Vasadi Figueroa and R. Ferer (October 2023).
- Pharma Manufacturing. Biologics, GLP-1s Driving Evolution of Fill-Finish Manufacturing (August 2026).
- Pharma Manufacturing. Novo Holdings Completes $16.5B Acquisition of Catalent (December 2024).
- U.S. Food and Drug Administration. FDA Clarifies Policies for Compounders as National GLP-1 Supply Begins to Stabilize.
- ISPE, Pharmaceutical Engineering. Visual Inspection Is Key to Ensuring Patient Safety in US Outsourcing Facilities (July/August 2025).
- A3P. Visual Inspections: Lessons from the ANSM Inspections, 2023 to 2025.
- Boon Logic. The CFO’s Guide to Inspection ROI (2026); Pharmaceutical Visual Inspection: Four Modalities, Four Financial Profiles (2026).
Further reading
Run the AVIS ROI Calculator · The CFO’s Guide to Inspection ROI